
Core Production Functions
Precise Batching and Metering: Independently and accurately weighs raw materials-such as aggregates (sand and gravel), cement, water, and admixtures-keeping errors within national standard limits to ensure mix compliance.
Efficient Forced Mixing: Utilizes a twin-shaft forced mixing unit capable of uniformly mixing various concrete types (ranging from dry-stiff to plastic mixes), ensuring high mixing efficiency and consistent product quality.
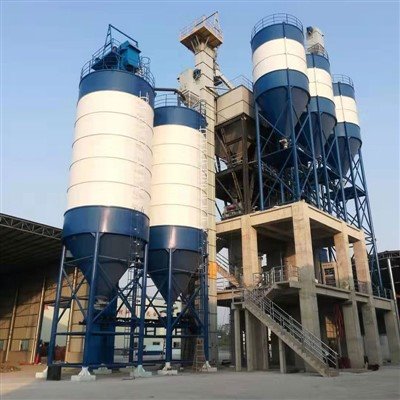
Continuous Batch Production: Delivers continuous output ranging from 25 to 240 cubic meters per hour (depending on specifications like HZS25–HZS240), meeting the high-volume material demands of large and medium-scale projects.
Supporting Auxiliary Functions
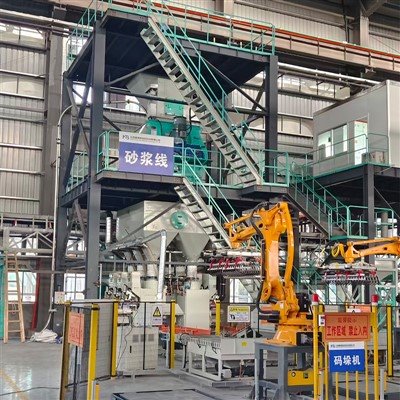
Automated Intelligent Control: Features a comprehensive control system that monitors production data in real-time, automatically compensates for aggregate moisture content, and transmits production reports remotely, significantly reducing human error.
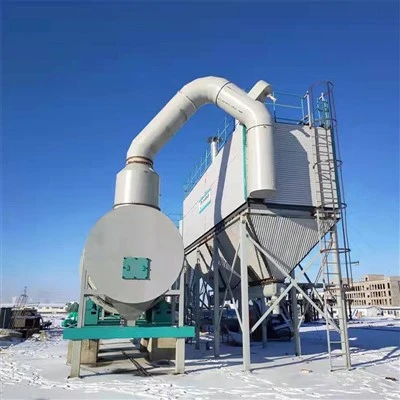
Eco-friendly, Low-pollution Operation: Employs fully enclosed powder conveying systems alongside high-efficiency dust removal and noise reduction devices to effectively minimize dust and noise emissions, meeting green construction standards.
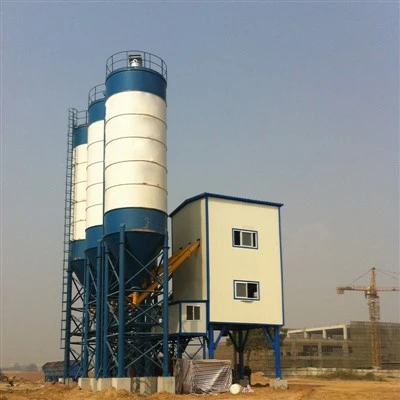
Flexible Application: Available in stationary and mobile configurations; stationary plants suit large commercial ready-mix facilities and long-term centralized projects, while mobile plants allow for rapid relocation, making them ideal for small-to-medium temporary construction projects.